Introduction
Injection grade PP copolymer is a thermoplastic raw material that combines impact resistance, processability and low density. It is widely used in the mass production of automotive components, durable packaging, household products, appliance parts and industrial containers. When the correct grade is selected, the material can support efficient mould filling, consistent cycle times and the mechanical performance required by the finished product.
Polypropylene is not a single, uniform material. The PP family includes homopolymer, random copolymer and impact copolymer grades, each offering a different balance of stiffness, clarity, toughness and temperature performance. Therefore, selecting a material simply because it is labelled “PP” is not enough. Product geometry, wall thickness, operating temperature, expected loads, surface quality and production speed must all be considered.
Burkasan contributes to circular production by recovering suitable plastic resources through controlled recycling processes. When recycled injection grade PP copolymer is considered, feedstock traceability, material consistency and application suitability become especially important. This guide explains the structure, benefits, applications, selection criteria and processing considerations of injection grade PP copolymer.
Contents
- What is injection grade PP copolymer?
- Main types of PP copolymer
- Properties and advantages
- PP copolymer vs PP homopolymer
- Common applications
- Injection moulding considerations
- Melt flow index and grade selection
- Common production defects
- The role of recycled PP copolymer
- Burkasan’s contribution to circular production
- Frequently asked questions
- Conclusion
What Is Injection Grade PP Copolymer?
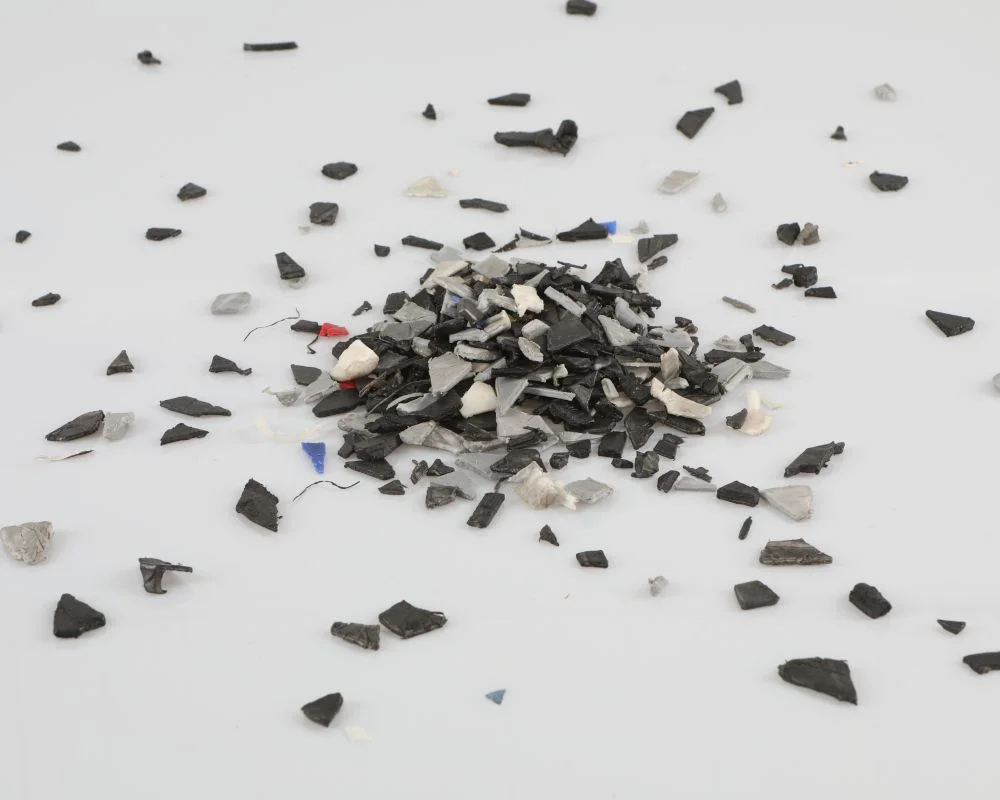
Injection grade PP copolymer is a polypropylene material produced by polymerising propylene with a controlled amount of another monomer, usually ethylene. Adding a comonomer can improve toughness and impact resistance compared with standard PP homopolymer. This makes the material suitable for components exposed to drops, impacts, vibration or low-temperature service conditions.
The term “injection grade” indicates that the material has a flow profile intended for injection moulding. During production, granules are fed into the machine, melted inside the barrel and injected under pressure into a mould cavity. The part is then cooled and ejected. Injection moulding enables manufacturers to produce complex geometries, fine details and repeatable dimensions in high volumes.
The performance of a grade cannot be determined from its polymer name alone. Melt flow rate, impact strength, tensile properties, density, additive package, colour and recycled content should also be reviewed. Material selection should therefore combine the technical data sheet, product requirements and a representative production trial.
Polypropylene can be processed through injection moulding, extrusion and blow moulding. More technical information about its characteristics and processing routes is available in the British Plastics Federation polypropylene guide.
Main Types of PP Copolymer
PP copolymers are generally divided into random copolymers and block or impact copolymers. In a random copolymer, the comonomer is distributed more randomly along the polymer chain. This structure may improve optical properties, flexibility and impact behaviour. Random copolymer grades can be considered when appearance, contact surfaces or balanced flexibility matter.
Block copolymers, also called impact copolymers, have a multiphase structure designed to improve toughness. They are frequently used for automotive components, crates, buckets, technical parts and durable consumer products because they provide a practical balance between stiffness and impact strength.
The right choice should not be based only on a “random” or “impact” description. Grade formulation, additives, fillers, colour and target mechanical values can significantly alter performance. Recycled grades also require consideration of feedstock history and sorting quality.
Colour can be another important selection factor, particularly for household goods, packaging and visible industrial components. For more information, manufacturers can review Burkasan’s solutions for coloured PP copolymer.
Properties and Advantages of Injection Grade PP Copolymer
One of the main advantages of injection grade PP copolymer is its ability to combine low weight with useful mechanical performance. With an appropriate product design, it may replace heavier plastic or metal solutions in selected applications. Its general chemical resistance, low moisture absorption and suitability for mass production further extend its range of use.
Key advantages include:
- Balanced resistance to impact and sudden loads
- Low density for lightweight product design
- Suitability for complex injection-moulded geometries
- Repeatable performance in high-volume manufacturing
- General resistance to many acids, bases and chemicals
- Compatibility with pigments, fillers and functional additives
- Availability of grades suitable for repeated flexing
- Potential use of recycled content when quality is controlled
Not every grade offers these benefits at the same level. Improving impact performance may reduce stiffness or change optical appearance. Products intended for prolonged outdoor exposure may require UV stabilisation. Food-contact, automotive, medical or electrical applications must use grades supported by the necessary declarations, test results and regulatory documentation.
PP Copolymer vs PP Homopolymer
PP homopolymer consists primarily of propylene units and is generally selected when stiffness, surface hardness and heat performance are important. PP copolymer is often preferred when a product requires greater toughness and impact resistance. Both material families can be processed by injection moulding, but their suitability depends on the actual service conditions.
Homopolymer may be appropriate for a rigid component that must retain its shape under load. A copolymer grade may be more suitable for a component exposed to low-temperature impacts or repeated drops. Technical comparisons similarly identify improved impact resistance as a key benefit of copolymer polypropylene.
Before selecting a grade, manufacturers should answer the following questions:
- Will the part be exposed to impact or accidental drops?
- Is stiffness or toughness the primary requirement?
- Will the finished product operate at low temperatures?
- Are gloss, colour consistency or transparency important?
- Does the design contain thin walls or long flow paths?
- Must the product comply with sector-specific standards?
- Is recycled content required by the customer or sustainability target?
These questions help define not only the polymer family but also the appropriate melt flow range, additive system and quality specification.
Common Applications
Injection grade PP copolymer is used across industries that require a combination of durability, light weight and efficient production. In the automotive industry, possible applications include interior trim, console parts, door components, protective housings and battery cases. These products may need to withstand vibration, assembly loads, temperature variation and occasional impact.
In packaging, common products include buckets, lids, transport containers, crates and durable storage boxes. Household applications include organisers, cleaning equipment, furniture components and appliance housings. Electrical and electronic products may use selected PP copolymer grades for protective enclosures and mounting components.
Typical application groups include:
- Automotive interior and exterior components
- White goods and small appliance parts
- Industrial crates, boxes and handling equipment
- Buckets, lids and reusable packaging
- Toys and sports equipment components
- Furniture fittings and plastic accessories
- Electrical and electronic housings
- Cleaning products and household goods
The same grade will not suit every application. A large crate may prioritise impact strength and long flow length, while a thin-wall lid may require easier flow and a shorter cycle. The real operating environment of the finished part must remain the starting point for grade selection.
Injection Moulding Considerations
A suitable raw material cannot compensate for an unstable process. When processing injection grade PP copolymer, barrel temperature profile, injection speed, holding pressure, screw speed, mould temperature and cooling time should be optimised together. Exact settings depend on the supplier’s data sheet, machine, mould, wall thickness and part geometry.
Processing guidance for polypropylene commonly presents mould temperatures across a broad range. A higher mould temperature may improve surface finish and dimensional stability but can also extend cooling and overall cycle time. These figures should only be treated as starting points. The technical recommendations for the selected grade should always take priority.
Polypropylene generally has low moisture absorption. Nevertheless, surface moisture, contamination or incompatible polymer residues may enter the material during storage and handling. Granules should be kept clean and protected, feeding equipment should be inspected, and adequate machine cleaning should be performed during colour or material changes.
Excessive melt temperature or residence time can cause degradation, odour, discolouration and reduced properties. A stable process window should be developed through controlled trials. If recycled PP copolymer is used, incoming inspection and lot-based production records become especially valuable.
Melt Flow Index and Grade Selection
Melt flow index, also called melt flow rate or MFI/MFR, describes how readily a molten polymer flows under standard test conditions. In general, a higher MFI can support easier filling of thin-wall parts or long flow paths. A lower MFI is associated with a different molecular structure and may provide a different mechanical profile. MFI is not an independent measure of quality, and a higher number is not automatically better.
The following factors should be assessed together when selecting injection grade PP copolymer:
- Part weight and wall thickness
- Flow length and runner design
- Required impact strength and stiffness
- Operating and storage temperature
- Dimensional tolerance and shrinkage expectations
- Colour, odour and surface appearance
- Recycled content target
- Food-contact or sector-specific compliance
- Production volume and target cycle time
Lot consistency becomes especially important for recycled material. Significant variation in flow behaviour can affect cavity filling, flash, part weight and mechanical performance. Manufacturers should request an agreed technical specification and carry out sample trials under conditions representative of mass production.
The material should also be evaluated as part of the complete product system. A technically suitable resin can still perform poorly if the gate design, cooling layout or wall-thickness transitions are inadequate. Early cooperation between the product designer, mould maker, processor and raw-material supplier can prevent expensive revisions.
Common Production Defects and Corrective Approaches
Short shots, warpage, sink marks, flash, flow lines, burn marks and colour variation are among the defects that may occur during injection moulding. In the case of incomplete filling, material flow, melt temperature, injection speed, venting and runner dimensions should be reviewed together. If flash develops, reducing pressure may not be sufficient; mould closing force, parting surfaces and material flow behaviour should also be examined.
Warpage and dimensional deviation may result from uneven cooling, part geometry or unsuitable packing conditions. Because polypropylene is semi-crystalline, temperature distribution inside the mould influences shrinkage. Sudden wall-thickness changes should be minimised, while ribs, bosses and fixing points should be assessed during the design stage.
Sink marks can occur where local sections are too thick or packing is insufficient. Flow lines may be influenced by melt temperature, injection speed, gate position and the way separate melt fronts meet. Burn marks can indicate trapped air, excessive speed near the end of filling or material degradation. Each defect should be investigated through controlled parameter changes rather than several simultaneous adjustments.
In recycled PP copolymer, incompatible polymer contamination, inadequate filtration or variation between colour lots may cause surface and mechanical defects. Production settings, raw-material lot numbers and quality-control records should be monitored together. This traceability helps distinguish material-related variation from mould or process problems.
The Role of Recycled PP Copolymer
Resource efficiency in plastics manufacturing is not limited to reducing part weight. Collecting, sorting, preparing and returning post-industrial or post-consumer plastics to production are also important components of a circular economy. When it meets the required specification, recycled injection grade PP copolymer can reduce the demand for virgin raw material in suitable products.
Recycled content cannot be introduced through the same formula in every product. Feedstock consistency, contamination, colour, odour, MFI, ash content and mechanical properties must be controlled. Applications that are safety-critical or regulated require additional verification. Clear technical communication between the recycler, compounder, processor and product owner is therefore essential.
Manufacturers may introduce recycled content gradually through trial batches and defined blending ratios. The finished parts should be assessed for dimensions, surface quality, impact performance, assembly behaviour and ageing. Results can then be used to establish a controlled production specification rather than relying on assumptions based solely on the resin name.
Circular design also considers the product’s next life. Mono-material structures, detachable connections and the avoidance of unnecessary coatings can simplify future recycling. Under this approach, PP copolymer is not merely today’s raw material; it can become a recoverable secondary resource at the end of the product’s service life.
Burkasan’s Contribution to Circular Production
Burkasan supports the return of suitable industrial and plastic resources to the economy through recovery and recycling activities. Controlled collection, separation and material-management practices create a stronger foundation for manufacturers evaluating more sustainable raw-material alternatives. For technical materials such as injection grade PP copolymer, reliable resource management directly affects the consistency of the final application.
When choosing recycled PP copolymer, manufacturers should assess more than price. Supply continuity, technical suitability, lot consistency, traceability and product requirements should all be considered. Burkasan’s circular-economy approach aims to keep recoverable plastics within the value chain and support more efficient use of resources.
This approach can also help businesses align material decisions with waste-reduction and sustainability objectives. The most effective outcome is achieved when environmental targets are translated into measurable technical criteria, controlled purchasing specifications and verified product performance.
Frequently Asked Questions
What does injection grade PP copolymer mean?
It is a PP copolymer grade with flow and processing characteristics designed for injection moulding. Copolymerisation, usually with ethylene, can improve toughness and impact resistance compared with PP homopolymer.
Is PP copolymer the same as polypropylene?
Polypropylene is the name of the broader polymer family. PP copolymer is a subgroup created by polymerising propylene with another monomer. Every PP copolymer is polypropylene, but not every polypropylene grade is a copolymer.
What is injection grade PP copolymer used for?
Common uses include automotive parts, battery cases, buckets, crates, lids, household products, toys, appliance components and electronic housings. The selected grade must match the impact, stiffness, appearance and temperature requirements of the part.
Is PP copolymer stronger than PP homopolymer?
Strength is not a single property. PP copolymer generally offers better toughness and impact resistance, while PP homopolymer often provides higher stiffness. The correct choice depends on the load, temperature and geometry of the application.
Is PP copolymer suitable for food contact?
Only grades with documented compliance for the intended food-contact use should be selected. The fact that a material is PP copolymer does not by itself demonstrate compliance. Additives, pigments, recycled content and migration requirements must also be checked.
What is the correct injection temperature for PP copolymer?
There is no universal setting. The correct barrel and melt temperatures depend on the grade, MFI, machine, mould, shot size and part geometry. The supplier’s technical data sheet should be used as the initial reference, followed by controlled production trials.
Does PP copolymer need to be dried?
Polypropylene has low moisture absorption and normally requires less drying than hygroscopic engineering plastics. However, drying or conditioning may be needed if surface moisture, poor storage or contamination is present. Supplier recommendations should be followed.
What happens when the MFI value increases?
In general, the molten material flows more easily, which can help fill thin-wall parts. Mechanical behaviour may also change, so MFI should be evaluated together with impact strength, stiffness and the other values in the technical specification.
Can recycled PP copolymer be injection moulded?
Yes. Recycled PP copolymer can be used in many injection-moulded products when it is properly sorted, processed and tested against the target specification. Representative trials and finished-part tests are particularly important for demanding applications.
Can PP copolymer be recycled?
Yes. Its thermoplastic structure allows it to be mechanically recycled after suitable collection and sorting. Mixing with incompatible polymers, fillers, labels, coatings or contamination can reduce the quality of the recovered material.
Conclusion
Injection grade PP copolymer is a versatile raw material that combines impact resistance, low weight, general chemical resistance and suitability for high-volume manufacturing. Reliable results depend on evaluating copolymer type, MFI, mechanical requirements, mould design and processing parameters as a complete system. When recycled content is used, feedstock quality, lot consistency, traceability and product suitability become central selection criteria. Through its recovery and circular-economy activities, Burkasan supports the return of plastic resources to the value chain and helps manufacturers consider more efficient and responsible material solutions.